International Fluid Power Inc.
International Fluid Power - Innovative Partners For Global Sourcing Of Fluid Power Products. Your Complete Hydraulic Source in SE Minnesota.
Choosing the right Chamfering Cutter is a process decision, not a catalogue decision. The cutter must match the material, edge angle, hole size, machine rigidity, and required surface finish. A 45-degree chamfer in aluminum behaves differently from the same operation in hardened steel. Coolant delivery matters too. So does spindle runout.
Market data shows why this choice deserves attention. Grand View Research estimates that the global cutting tools market reached approximately USD 23.5 billion in 2023. Its report also projects continued growth through 2030, driven by automation, aerospace production, and precision machining. The U.S. Cutting Tool Institute and Oxford Economics reported about USD 2.61 billion in U.S. cutting-tool consumption during 2023. These figures suggest strong demand, but they do not guarantee the right tool for every job.
Dr. Scott Smith, a recognized machining researcher and co-author of Machining Dynamics, offers a useful principle: “Tool selection is a process, not a product decision.” That idea should guide every Chamfering Cutter comparison. Examine carbide grade, coating, flute geometry, shank tolerance, and chip evacuation. Then test the cutter on the actual machine. A catalogue cannot reveal vibration at 8,000 rpm. It cannot predict a burr on a thin-wall component. This is where experience becomes measurable. Record cycle time, tool wear, burr height, and finish. The first choice may be wrong. That is not failure; it is evidence for a better decision.
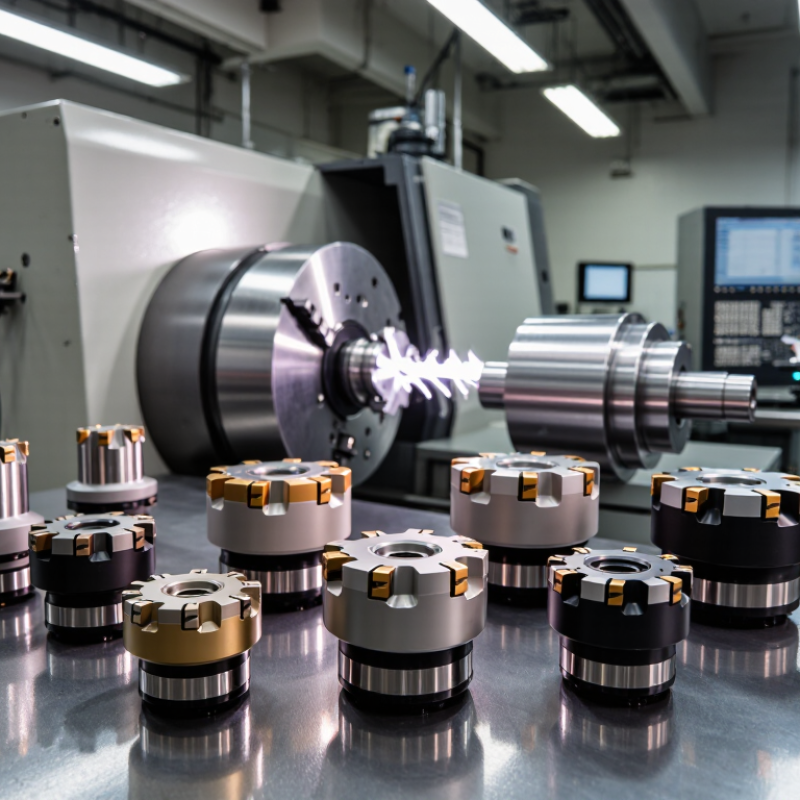
Understanding chamfering cutters starts with the edge they must create. A chamfering cutter removes material at a controlled angle, often 45 degrees, to soften sharp edges, guide assembly, or prepare a hole for countersunk hardware. In daily machining, I check the drawing, workpiece hardness, chamfer width, and available spindle speed before selecting a tool. Small details matter. A 0.5 mm edge break needs different control from a 3 mm chamfer.
Industry data supports this careful approach. The 2024 Global Machine Tools Market report estimates that computer-controlled equipment represents more than half of new machine-tool demand. This shift increases the value of repeatable cutter geometry and stable tool holders. Another 2023 machining productivity survey reported that tool changes and setup work can consume over 15% of production time. Choosing one cutter for several compatible operations may reduce interruptions, but that assumption can fail on hard alloys.
For aluminum, a sharp carbide cutter usually produces a cleaner edge with less built-up material. For stainless steel, a tougher geometry and steady feed can reduce chipping. Coated tools may extend working life, although the result depends on speed, coolant, and operator control.
I have sometimes selected a larger diameter to improve stability, then found that access became worse. That mistake is easy to repeat. Inspect the finished chamfer under good lighting, measure its width, and watch for burrs, uneven marks, or vibration lines before approving the setting.
Start with the material. A cutter for aluminum should clear soft, sticky chips quickly, while one for carbon steel needs stronger edges and controlled heat resistance. Stainless steel demands extra care because excessive rubbing can harden the surface. Plastics require sharp cutting edges, generous clearance, and moderate cutting pressure to prevent melting.
Match the cutter angle to the drawing, not to habit. A 45-degree chamfer is common, but a different angle may protect a sealing edge or guide assembly. Measure the edge. The cutter diameter should suit the available space and required chamfer width. A large tool can improve stability, yet it may strike nearby features. Flute count also matters. Fewer flutes often provide better chip room in aluminum, while more support can help during steel machining.
In practice, I check the rake, relief, and workholding before changing speed or feed. A dull edge can make a good geometry appear unsuitable. Small details matter. Secure clamping reduces chatter, especially on thin parts. Use a test cut on scrap material, then inspect the width with a gauge or microscope. I still recheck the first production piece, because tool deflection and machine rigidity can change the result. No catalog chart replaces that observation. A slightly conservative setting may leave a cleaner edge, though it can reduce productivity. That trade-off deserves honest review.
How to Choose the Right Chamfering Cutter?
Selecting the correct cutter size starts with the chamfer width, material, and available clearance. For a 1 mm chamfer, a compact cutter usually gives better control than an oversized tool. Oversized cutters can increase cutting force and leave visible witness marks. Measure the actual edge, not only the drawing. A 2024 global manufacturing survey reported that 88% of producers are increasing digital process monitoring, but basic measurements still prevent many shop-floor errors.
The angle must match the drawing and the cutter’s intended geometry. A 45-degree cutter suits common deburring work, while 60-degree or 90-degree angles may support countersinks or special edge profiles. Check the included angle, not just the catalog description. ISO 13399 recommends consistent cutting-tool data, which helps compare diameter, flute length, and cutting geometry across suppliers. Still, catalog numbers can confuse inexperienced users.
Shank selection affects rigidity. Match the shank diameter to the holder, then keep tool projection as short as practical. A longer setup may reach the feature, but it can amplify chatter beside a thin wall. For high-speed machining, review runout and balance data before increasing spindle speed. A 2023 industrial tooling report linked improved tool-life monitoring with lower unplanned downtime, though results varied by material and machine condition. I would still test one cutter first. The first trial is rarely perfect. Record sound, burr shape, edge finish, and tool wear after each pass.
| Cutter Size (Cutting Diameter) | Included Angle | Typical Shank Diameter | Typical Starting Chamfer Width | Suitable Applications | Material Guidance | Selection Notes |
|---|---|---|---|---|---|---|
| 6 mm | 45° | 4 mm or 6 mm | 0.3–1.5 mm | Small deburring operations, narrow edges, compact parts, and light CNC work | Aluminum, brass, plastics, and mild steel with light feeds | Use when access is limited or when a small, controlled edge break is required. Check that the tool holder can grip the small shank securely. |
| 8 mm | 45° | 6 mm or 8 mm | 0.5–2.0 mm | General-purpose edge breaking on small to medium components | Aluminum alloys, brass, engineering plastics, and low-carbon steels | A practical choice for moderate rigidity and good access. Avoid excessive radial engagement on hard materials. |
| 10 mm | 45° | 6 mm or 8 mm | 0.8–2.5 mm | General machining, hole deburring, and preparation of weld or assembly edges | Aluminum, steel, cast iron, and stainless steel when appropriate cutting data is used | Provides a useful balance between reach, rigidity, and cutting capacity for many standard jobs. |
| 12 mm | 60° | 8 mm or 10 mm | 1.0–3.0 mm | Moderate countersinking, angled edge preparation, and parts requiring a steeper chamfer | Aluminum, steel, stainless steel, and nonferrous metals | Confirm the required included angle before cutting. A 60° cutter produces a different profile from a standard 90° countersink. |
| 12 mm | 90° | 8 mm or 10 mm | 1.0–3.0 mm | Standard countersinking for flat-head screws and larger edge chamfers | Aluminum, mild steel, cast iron, and stainless steel with suitable speeds and feeds | For a 90° included angle, the two cutting faces are typically 45° to the work surface. Verify the fastener specification when countersinking. |
| 16 mm | 45° | 10 mm or 12 mm | 1.5–4.0 mm | Large edge breaks, robust deburring, and heavier machining on rigid machines | Steel, cast iron, stainless steel, and aluminum | The larger diameter supports wider chamfers but requires more machine clearance and adequate spindle power. |
| 20 mm | 90° | 12 mm | 2.0–5.0 mm | Large countersinks, heavy edge preparation, and high-volume production work | Steel, cast iron, and aluminum on rigid milling or CNC equipment | Use a rigid setup and short tool projection. Start with a conservative feed and adjust after checking finish and tool load. |
| 25 mm and above | 45° or 90° | 12 mm or larger | 3.0–6.0 mm or more | Large structural components, broad edge preparation, and specialized countersinking | Steel, cast iron, aluminum, and other machinable metals | Confirm machine capacity, holder compatibility, maximum speed, and required cutting depth. These tools are generally unsuitable for light hand-held use. |
Selection note: The listed chamfer widths are typical starting ranges rather than universal limits. Final selection should be based on the required edge size, workpiece material, machine rigidity, tool material, holder compatibility, and the cutter manufacturer’s cutting data.
Evaluating Tool Materials, Coatings, and Cutting Performance
Choosing a chamfering cutter starts with the workpiece, not the catalog. High-speed steel suits softer metals and interrupted hand-fed work. Carbide usually holds its edge longer in production machining. It also demands a rigid setup. On a flexible machine, carbide can chip before its hardness helps. Rigidity matters.
Coating selection should match heat, friction, and material. A titanium-aluminum nitride coating can support dry cutting and elevated temperatures. A lower-friction coating may help when aluminum sticks to the cutting edge. Coatings do not repair poor geometry. I have seen a coated tool fail quickly after excessive feed and weak clamping. Check the cutter angle, flute count, edge preparation, and runout before blaming the coating.
Cutting performance is visible in more than surface shine. Watch spindle load, burr size, sound, and chamfer width after several parts. Start with conservative speed and feed values from the tool maker. Then adjust one variable at a time. Keep the tool overhang short. Use coolant when the material and coating allow it. Small batches need a practical compromise between tool life and cycle time. A perfect laboratory result may not survive a real fixture. Measure parts with a gauge or optical comparator, and record edge wear. Sometimes the cheaper cutter wins, but only after setup time is counted. Measure the edge.
How to Choose the Right Chamfering Cutter?
A chamfering cutter should match the machine before it touches the workpiece. Check the spindle interface, maximum speed, available power, and tool clearance. A cutter may fit physically but still perform poorly under load. Confirm the cutter’s diameter and angle against the machine’s limits. I have seen oversized tools create vibration on otherwise rigid equipment. That mistake wastes time and can damage the cutting edge.
Workholding deserves equal attention. Secure the part close to the cutting area, especially when removing a wide edge. Soft jaws, clamps, or a fixture should prevent movement without distorting thin material. Check for chips beneath the part. Even a small chip can tilt the workpiece and produce an uneven chamfer. Leave enough access for the cutter, but avoid excessive overhang. Shorter setups usually feel more stable.
Tips: Test the setup on scrap material. Start near the lower recommended speed and feed. Watch the sound, chip shape, and surface finish. Adjust one variable at a time. Coolant choice also matters, though I sometimes overlook it during quick jobs. Recheck the edge after several passes, because heat and tool wear can change the result. Steady clamping and realistic cutting conditions matter more than chasing maximum speed.
Checking machine compatibility, workholding, and operating conditions
This is an example of a widget area that you can place text to describe a product or service. You can also use other WordPress widgets such as recent posts, recent comments, a tag cloud or more.
© 2025 International Fluid Power, Inc. All Right Reserved.